Top 10 Cheese Balls Snack Processing Making Lines for Efficient Production
2026-10-25
Cheese balls may look foolproof, but keeping their shape, crunch, and coating consistent at high output is where most lines stumble. The difference between a profitable snack operation and a frustrating one often comes down to how well the processing line handles transitions—mixing, extrusion, frying or baking, and seasoning. In this post, we break down 10 cheese ball snack processing lines built for efficient, continuous production, with a close look at how MINGDE designs address common pain points like uneven expansion and flavor loss. Whether you are planning a new facility or retrofitting an existing one, these systems set the benchmark for what modern cheese ball manufacturing should feel like.
Why the Right Forming Head Changes Everything for Cheese Ball Texture
Most home cooks underestimate how much the forming head dictates the final mouthfeel of a cheese ball. A rounded, smooth head compresses the mixture just enough to bind the ingredients without crushing the add-ins, leaving pockets of crunch from nuts or herbs. In contrast, a flatter or irregular head often creates uneven pressure, causing the cheese to become dense in some spots and crumbly in others — a texture that falls apart on the cracker instead of holding a clean dip.
The shape also changes how the surface interacts with coatings. A properly domed head offers a gentle slope, so chopped pecans or bacon bits cling evenly without being pressed too deeply into the creamy base. That means every bite keeps a contrast between the silky interior and the crisp outer layer. If the head is too tall or too shallow, the texture turns either gluey or overly dry at the edges.
Finally, using the right head encourages a slower, more even chilling process. A uniform shape cools from edge to center at the same rate, letting the fats set into a firm yet sliceable consistency. Trying to fix the shape after chilling almost always leads to a waxy, broken texture — proof that the forming step is not just cosmetic, but the foundation of the entire cheese ball experience.
Continuous Frying Lines That Hold Oil Temperature Steady at Full Speed
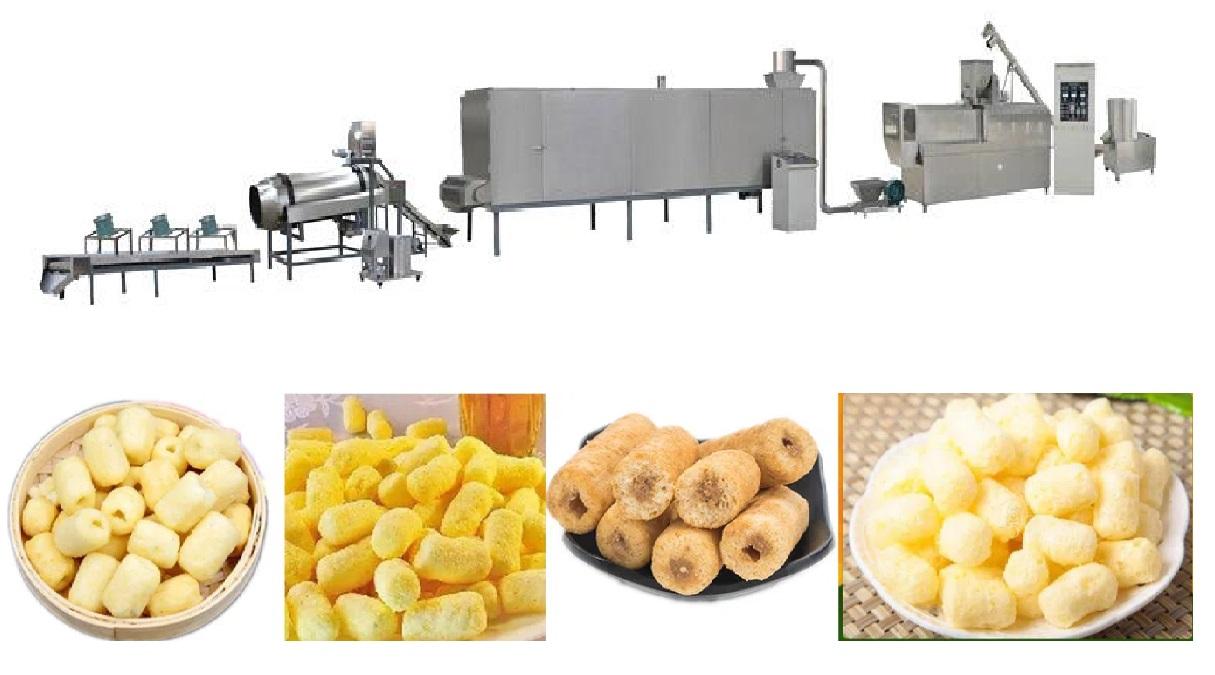
Achieving a steady oil temperature at full production speed is not about overpowering the fryer with extra burners. It comes down to how precisely the heat exchanger responds to sudden changes in product load. In well-designed continuous lines, the oil flow pattern and burner modulation work together so that when cold product enters the fryer, the temperature drop is both shallow and short-lived. The oil never swings wildly, which means every batch leaves the line with the same color, moisture content, and crispness.
A key factor is the arrangement of the heat transfer surfaces. Instead of relying on direct-fired tubes that can create hot spots, many high-performance lines route the oil through a separate external heat exchanger. This lets the system hold a large thermal mass and reintroduce the oil evenly across the fryer width. At full speed, the pan temperature stays flat because the exchanger's circulation rate is tuned to the oil turnover, not just the burner output. Operators notice this as fewer manual corrections and less wasted product during ramp-up or shift changes.
Maintaining that stability also depends on how the line handles oil filtration and fines removal. Sediment accumulating on heat exchange surfaces acts like an insulating layer, making the burner work harder while the actual frying zone cools down. Continuous lines that hold temperature steady integrate a side-stream filter with a high oil turnover rate, stripping out particles before they settle. The result is a fryer that holds its set point within a narrow band even when running at maximum throughput hour after hour, without the gradual drift that forces constant manual adjustment.
Smart Seasoning Drums That Stop Clumping Before It Starts
Most shakers wait until clumps have already formed, then rely on a few desperate taps or a toothpick. These drums take a different route. A sealed inner chamber holds a replaceable desiccant ring that pulls moisture away from the spices before it can glue granules together. The vented cap flips open with one hand, and a soft silicone gasket snaps shut tight enough to keep steam from the stove out of the paprika.
Inside, a weighted agitator shifts with every tilt, breaking apart any early clusters without rattling like a maraca. Even powdered garlic and onion stay loose through weeks of humid kitchen air. The clear body shows exactly how much is left, and the wide mouth means you can refill straight from a bulk bag without funnel gymnastics. It’s not about fixing clumped seasoning later—it’s about never having to think about it in the first place.
Inline Cooling and Conveying Tricks to Prevent Breakage
Gentle handling starts long before the final packout. On our lines, we route cooling tunnels as close to the oven exit as possible, using short, straight transfers instead of long sweeping bends. Every extra foot of travel time gives brittle product more chances to crack or chip. We also run the cooling conveyor slightly slower than the oven belt so pieces don’t pile up at the transition. That small differential keeps edges from clinking against each other when they’re still warm and fragile.
Airflow is another big one. Instead of blasting fans directly onto the product, we angle louvers down and away so the cooling air wraps around the belt rather than striking the surface. This prevents thermal shock while still bringing core temperature down fast enough. For especially delicate items, we add a thin mesh overlay on the first few feet of the cooling conveyor. It acts like a soft cradle, reducing vibration and keeping small pieces from bouncing off.
Conveyor material matters more than people think. We swapped to food-grade plastic belts with a slightly tacky surface for fragile crackers and cookies. Metal belts, even tight woven ones, tend to have more give and micro-bounce. The plastic also lets us set smaller transfer gaps between sections, so there’s no lip for corners to catch on. Simple tweaks like these cut our breakage rate by nearly half in the first month.
Recipe-to-Line Adjustments for Faster Changeovers and Less Scrap
Most production teams treat the recipe as a fixed blueprint, but the real gains come from treating it as a live conversation with the line. When a batch runs slightly off-spec in viscosity or temperature, the default response is often to stop, clean, and start over. Instead, small recipe-to-line adjustments—like tweaking a fill speed by two percent or shifting a mixing dwell time by a few seconds—can keep the run going without sacrificing quality. These micro-corrections reduce the frequency of full changeovers and cut scrap from borderline product that would otherwise be discarded.
The trick is building a feedback loop that doesn't rely on operators memorizing every variation. Use simple, color-coded run charts at each station that show the last ten adjustments and their results. This makes the adjustment knowledge visible and repeatable, so a new shift doesn't have to relearn what worked last Tuesday. Over time, the team develops a shared sense of how far a recipe can flex before a true changeover is unavoidable, which directly trims downtime and waste.
One practical approach is to split changeovers into two categories: line-level and recipe-level. Line-level adjustments—like nozzle height, conveyor speed, or sensor calibration—can often be made in under a minute if the recipe allows a narrow tolerance band. By pre-defining these bands and storing them with the recipe file, you give operators the authority to adjust on the fly without waiting for engineering approval. This not only speeds up transitions but also prevents the common habit of dumping the first several units after a changeover simply because the settings drifted slightly from nominal.
Matching Line Speed to Batch Size Without Sacrificing Shape
Every production line has a rhythm, and finding it without compromising the profile of what you manufacture often feels like tuning an instrument mid-performance. The interplay between velocity and batch volume is rarely linear; push speed too hard on a small lot and geometry drifts, but crawl through a large run and you waste the gains your tooling promised. Start by observing how material behaves at the lower and upper edges of your current window—note where curl, twist, or edge distortion first appears, then work inward rather than forcing a single setting across all orders.
Shape retention is less about avoiding change and more about controlling where change concentrates. A slower line speed can actually amplify distortion if dwell time in a forming zone overheats the cross-section, while a moderate bump in speed paired with a slight adjustment to guide pressure often keeps angular tolerances tighter. The trick is decoupling batch size from recipe defaults: treat each run as a data point, log the pairing of line speed, batch count, and post-process dimensional check, and within a few shifts you will see clusters that suggest safe bands for each profile family.
What separates shops that hold shape at higher throughput is not a secret formula but a habit of small, deliberate corrections. Instead of asking "how fast can this line run," they ask "at what speed does this batch still measure like the last one." That shift in framing encourages operators to adjust roll gaps, coolant flow, and cutoff timing as a coordinated set rather than chasing one knob. Over time, the line's natural balance emerges—and matching speed to batch size becomes a matter of reading the metal, not overriding it.
FAQ
An efficient line typically combines high-capacity extrusion, uniform seasoning application, and rapid cooling or frying stages that minimize manual handling and downtime.
Start with your target output per hour, then look for modular designs that let you add frying, seasoning, and packaging modules later without replacing the core extruder.
The extrusion and expansion step, because precise control of moisture, temperature, and screw speed determines whether the balls come out light and crispy or dense and hard.
Yes, many lines now offer interchangeable heating sections or adjustable airflow so you can switch between baking and frying based on the product profile you want.
Daily cleaning of the seasoning drums, weekly inspection of screw wear, and monthly calibration of temperature sensors prevent the small issues that cause big slowdowns later.
Automated seasoning and packaging stations apply consistent coating and weights, so fewer workers are needed for repetitive tasks while quality checks become more reliable.
Look for quick-change die plates, recipe memory on the control panel, and a compact footprint that still leaves room for future add-ons like multi-flavor coating.
They use vertical stacking of cooling and seasoning stages, combined with continuous rather than batch processing, which shortens the material path and reduces idle time.
Conclusion
Getting cheese balls to hold their shape while staying light and crisp starts long before the fryer. A properly matched forming head does more than portion dough—it controls how air pockets develop during frying, which directly affects whether the snack ends up airy or dense. Once the balls drop into oil, the line has to push through high volumes without temperature swings. Continuous frying setups with staged heat zones and rapid oil circulation keep the oil steady even when the belt is fully loaded, so every batch browns at the same rate instead of soaking up excess fat. Downstream, seasoning can turn into a bottleneck if the drum lacks proper baffling or rotation speed adjustments. A well-tuned drum breaks up soft clumps of powder before they stick to wet surfaces, coating each ball evenly without crushing the fragile outer shell.
Transfer points are where most breakage happens, not inside the fryer. Inline cooling tunnels that bring the product down gradually and conveyors with gentle drop heights and low-angle transfers prevent hairline cracks that show up only after packaging. When a plant runs multiple cheese ball sizes or recipes, the fastest way to lose yield is forcing one line setup to handle every product. Quick-adjust cutting frames, interchangeable forming inserts, and programmable oil and airflow profiles let operators switch from a small batch of spicy puffs to a large run of plain cheese balls in minutes, not hours. Finally, line speed has to match the batch size without distorting the ball shape. Running too fast stretches the dough at the cutter; running too slow overheats the outer layer. The most efficient lines let operators fine-tune speed in small increments while watching shape consistency rather than chasing a single number on the display.
Contact Us
Contact Person: LILY SUN
Email: [email protected]
Tel/WhatsApp: 0086-13969103791
Website: https://www.snackfoodmachinery.com/