Precision Metal Bracket Supplier Qualities That Ensure Reliable Performance
2026-11-22
In precision manufacturing, a metal bracket is rarely the most visible component, yet it often determines whether an assembly holds up under stress, vibration, or long-term wear. The difference between a bracket that quietly does its job for years and one that fails early usually comes down to the supplier behind it. At BOSI, we have seen how tighter tolerances, consistent material sourcing, and honest communication turn a simple bracket into a dependable load-bearing link. This post breaks down the supplier qualities that actually protect your product's performance, so you can make sourcing decisions with confidence instead of hoping for the best.
Tolerances That Hold When the Line Finally Runs at Full Speed
Once the line stops lurching through trial cycles and settles into full-speed cadence, tolerances start behaving differently. Heat from motors, spindle bearings, and friction surfaces soaks into frames and rails, so dimensions that were stable during a slow runoff can wander by the middle of a shift. The tolerances that matter are not the ones taken on a cool machine after lunch; they are the ones that survive thermal saturation and cyclic loading hour after hour.
Some of the worst drift hides in details that look harmless at standstill. A few microns of growth in a bearing housing changes preload, and that shift travels straight into a sealing face or a cutting edge. Rather than tightening every callout on the drawing, it makes sense to isolate the dimensions that carry the process under speed: tool mount concentricity, flatness across the clamp area, and the repeatability of locating features that absorb impact on every cycle. Those are the numbers that determine whether small variation stays random or turns into scrap by the second break.
One check that gets skipped too often is to measure cold-start geometry, run the line at full rate until temperatures stabilize, and measure again without stopping. The gap between those two readings shows where the process actually lives. If the tolerance band cannot absorb that shift, no amount of static inspection in a lab will save the run. Full-speed tolerance is a different specification from standstill accuracy, and treating it separately prevents most of the launch-week arguments about parts that measured perfectly at rest but drift once the line finds its rhythm.
Material Traceability That Goes Deeper Than a Generic Cert
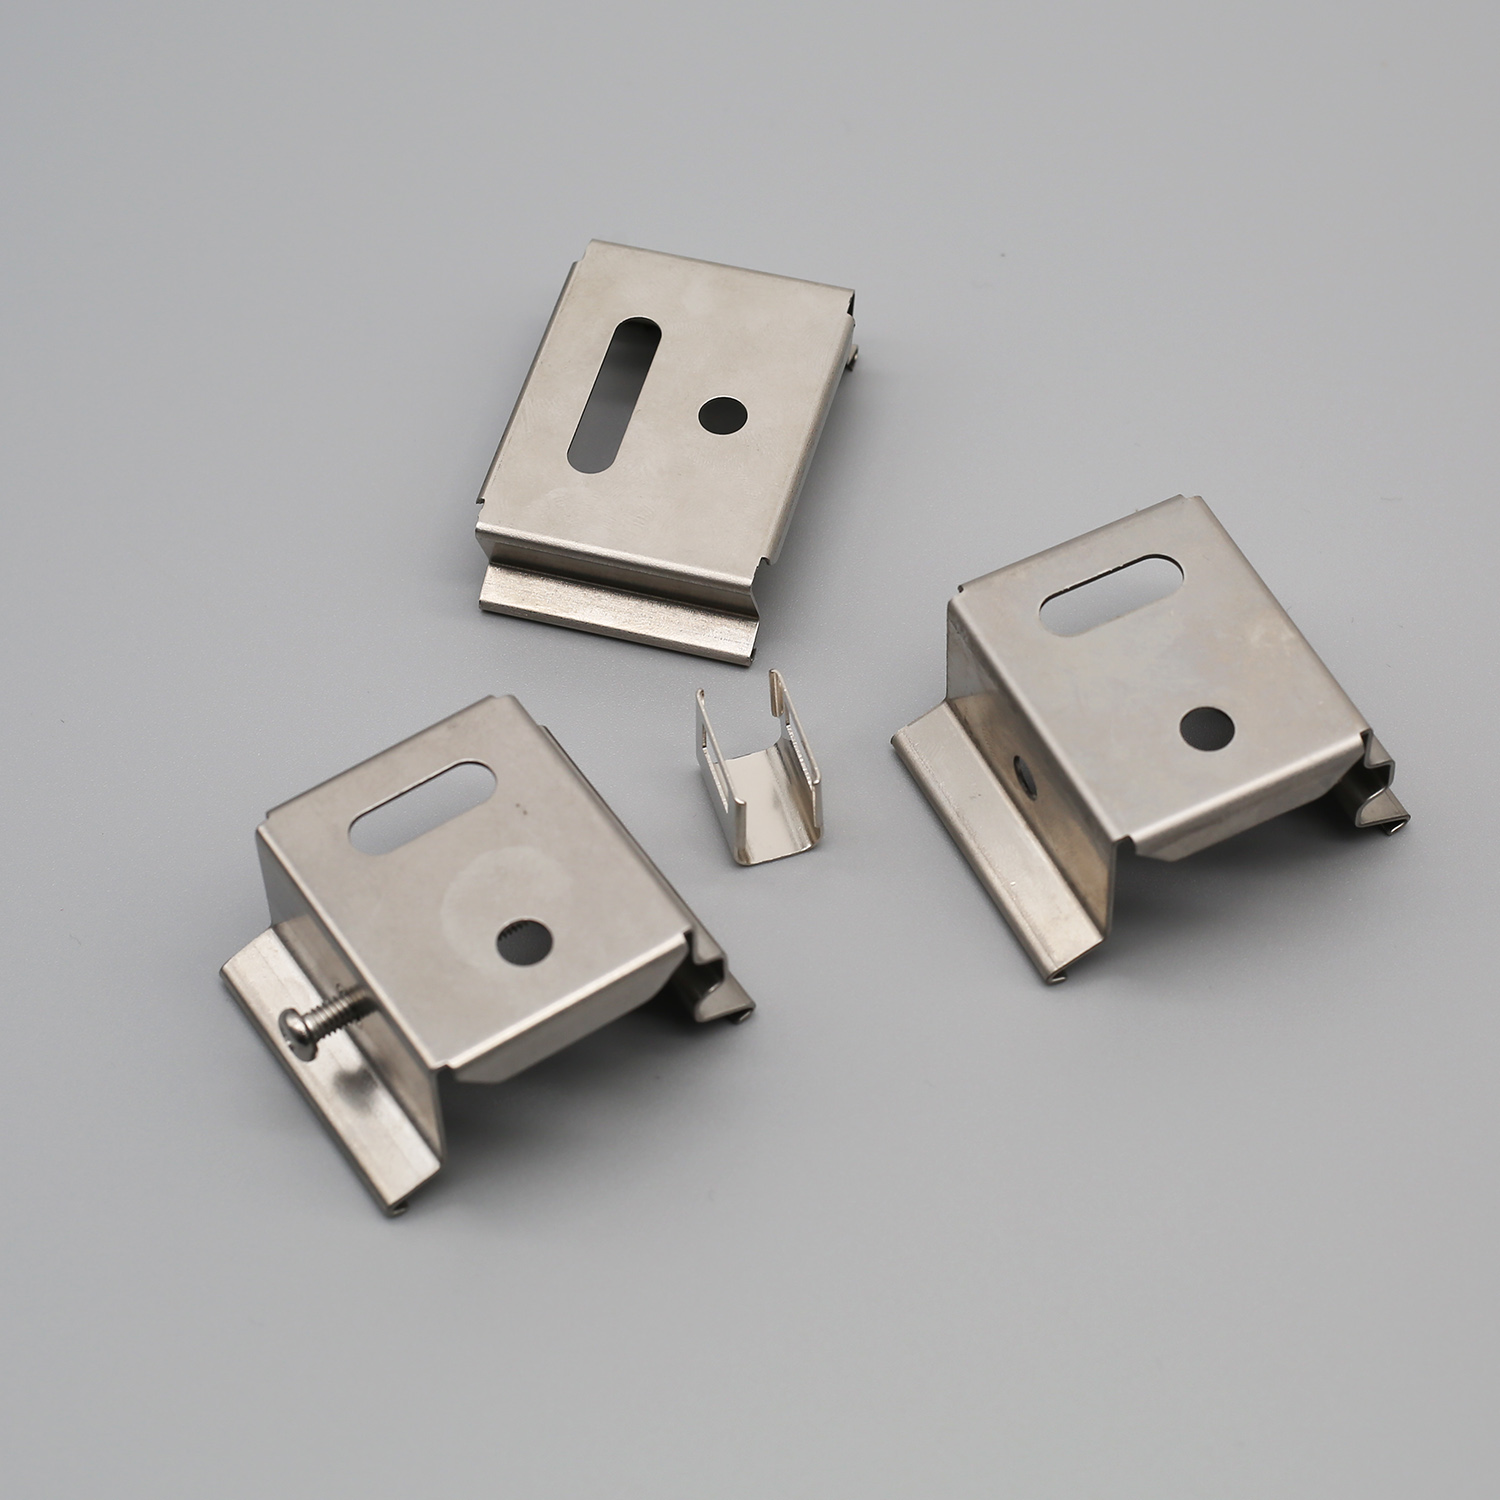
Most suppliers will hand you a PDF with a mill name and a heat number, then call it traceability. We treat that as the starting line, not the finish. Every batch we move is tied to the original pour, the slitting line, the coating run, and even the specific operator shift—because when something fails in the field, you shouldn’t have to guess which of five identical coils actually left the warehouse.
That level of detail doesn’t live in a single certificate. It lives in our internal lot genealogy: a running record that connects incoming chemistry data, processing temperatures, surface roughness readings, and final dimensional checks to the exact roll or bundle number you receive. Ask us about a claim two years later, and we can pull the full journey in minutes—not days of back-and-forth emailing.
What sets this apart from a generic cert is the ability to act on the data. If a particular cast shows an outlier in elongation, we can quarantine only the affected cuts instead of issuing a blanket recall. If your forming operation struggles with springback, we can trace it back to yield strength variation across a single heat and adjust future orders. The certificate tells you what the material was supposed to be; we show you what it actually did, from melt to dock.
Finishes That Do Not Fade Between the Sample and the Shipped Order
There is a particular frustration in unboxing a production piece and noticing the color has shifted just enough to feel off from the swatch you approved. We keep that from happening by pulling finish materials from the same pigment batches used for your signed sample, then mixing them in small, controlled runs rather than large seasonal batches. The result stays closer to the original, even under different lighting on a showroom floor.
Certain tones, especially muted greys, deep blues, and warm off-whites, are more prone to drifting when fillers or recycled content fluctuate. Our finishing team adjusts the base coat and topcoat ratio per color family instead of relying on one standard formula. That means the sheen level and undertone you see on the sample board are what get sealed into the final order, without a surprise shift toward greener or chalkier.
We also keep retained panels from each finish lot, so if a future order needs to match an earlier delivery, the reference is a physical production part rather than a digital color file. This closes the gap between an attractive first sample and the piece that actually arrives on site.
Engineering Answers Before a Tolerance Question Becomes a Delay
In a machine shop, the drawing is the first place a schedule either holds together or quietly falls apart. The tolerances that nobody calls out at the review meeting do not disappear; they resurface as a paused operation, a phone call to the designer, or a pile of parts waiting on a clarification. Engineering answers before the question turns into a delay by marking the intent on the print while the part is still lines on a screen.
Unresolved tolerance issues tend to hide in the handoffs. One team assumes the mating part controls position, another reads the datum differently, and the supplier bids what they think they can hold. Each assumption adds days that never show up on the critical path until they already have. A short note about allowable variation, fit condition, or inspection method costs minutes at the start and prevents a stalled release later.
The most useful habit is to review the drawing as if you are the person setting up the machine, not the one creating the model. Walk the interfaces, ask where the burr can live, how plating changes the size, and which surfaces locate the part in assembly. When those decisions are captured in the tolerance block before procurement sees the package, the drawing stops being a request for interpretation and starts being a set of instructions.
Capacity That Flexes Without Turning Your Schedule Into a Gamble
Most scheduling tools ask you to predict the unpredictable, then punish you when reality wanders off script. That tension disappears when capacity moves in smaller, more responsive blocks. Instead of locking a full shift weeks out, you adjust in near real time—adding coverage where volume is actually building, trimming it where the floor has gone quiet—without triggering a cascade of understaffed gaps or overtime surprises.
The difference comes down to guardrails, not guesswork. The system watches incoming demand signals, leave requests, and staff availability, then suggests moves that keep service levels steady. If a change would violate a contract rule or stretch a team too thin, it flags that before the schedule is published. You get to say yes to a shift swap or an extra pair of hands without wondering whether next Tuesday will fall apart.
That kind of controlled flexibility changes the conversation with staff, too. People can pick up hours that fit their week, managers can approve changes without rebuilding from scratch, and the schedule stops feeling like a brittle promise. It becomes a working plan—one that bends where it should, stays firm where it matters, and never asks you to bet the day on a forecast you were never given.
Final Checks That Catch What the Drawing Alone Cannot
A diameter can look perfectly controlled on a clean sectional view and still bind once weld distortion, plating buildup, and hand-tightened assembly tolerances enter the picture. That is why the last pass stops trusting nominal geometry and starts checking the part as it actually sits in the assembly. Mating faces get checked for flatness after surface treatment, aligned holes are probed on a first article, and running clearance is confirmed with a physical shim rather than a screen measurement. These are the checks that surface when the part has real weight, real finish, and real tolerance stack.
The drawing often implies ideal conditions: the fastener seats square, the seal compresses evenly, the connector reaches its mate without strain. Final checks probe the edges instead. Can the bolt be installed with standard tool access once the adjacent bracket is in place? Does the gasket actually deflect enough under clamp load, or does the housing bottom out first? Does the wire harness have enough slack when all related features sit at worst-case tolerance? Walking through the assembly sequence with hardware in hand tends to expose interference and accessibility problems that no orthographic view flags.
Some defects never show up until the part is handled. A sharp edge reads clean on paper but feels wrong under a thumb. A latch may look fully engaged while its pawl only half-seats. A machined bore can measure in tolerance yet still gall a pin because of surface finish or break-edge condition. These tactile and functional trials catch what the drawing cannot describe, not because the drawing is careless, but because physical behavior is always less polite than geometry.
FAQ
Start with their tolerance capabilities and whether they can hold the dimensions your design actually requires. Ask for sample parts or a small pilot run, and pay attention to how they handle edge deburring, flatness, and hole positioning. A good supplier will also flag potential manufacturing issues before production starts instead of waiting for the parts to fail inspection.
Brackets often act as alignment points or load-bearing mounts, so even a small deviation can cause assembly misalignment or stress concentrations. A supplier that controls tolerance consistently across the batch means you won't have to sort parts on the line or rework enclosures later. It's less about the nominal dimension and more about repeatability from the first bracket to the last.
It depends on the environment, but stainless steel, cold-rolled steel, and aluminum alloys cover most structural and corrosion requirements. Finishes such as zinc plating, anodizing, or powder coating add surface protection, but the prep work matters just as much. Ask how the supplier cleans parts before finishing because poor adhesion or trapped moisture can shorten service life quickly.
Look for evidence that inspection is tied to the process, not just the final box. That might mean in-process checks after laser cutting or bending, documented first-article inspection reports, and clear lot traceability. A trustworthy shop will share nonconformance data or corrective actions without making you ask twice, because they're already using that information to improve their own workflow.
Prototyping reveals how a supplier interprets your drawings and how well they communicate when something is unclear. It also shows whether they can move from a prototype to production without changing the part's fit or finish. Use a small batch to test not only the bracket itself but also their consistency, packaging, and handling.
Neither one should be considered in isolation. A low price and fast turnaround won't help if the brackets arrive out of specification or with burrs that damage mating surfaces. Compare total cost of quality, including sorting time, line stoppages, and returns, and look for a supplier that gives realistic dates and hits them consistently.
Watch for vague tolerance discussions, no formal drawing review, or an inability to explain how they control variation in bending and hole placement. If a supplier quotes without asking about material grade, finish requirements, or how the part is used, that's often a sign they're treating it as a commodity rather than a precision component.
Share updated drawings quickly, give feedback on what works and what doesn't, and involve them early when a design is still flexible. Regular communication about upcoming demand helps them plan material and capacity. In return, ask for periodic process data or sample inspection results so you can catch small shifts before they turn into field failures.
Conclusion
A precision metal bracket supplier earns trust long before the first shipment reaches the dock. The real test is whether tolerances stay consistent when production shifts from a careful prototype run to full-speed output, and whether the shop can back that consistency with material traceability that goes deeper than a generic cert. You want heat numbers, revision details, and test data tied to the exact lot, not a paper that simply says the alloy is “certified.” Finishes matter just as much as dimensions. The coating on the sample should look and perform the same on the shipped order, without drift in thickness, adhesion, or edge coverage. When those details line up, the brackets drop into place without rework or finger-pointing later.
Strong suppliers also answer engineering questions before a tolerance issue turns into a stalled line. That means reviewing the drawing enough to flag form, fit, or fixturing concerns early, and having capacity that flexes with demand rather than forcing your schedule into a gamble. It also means final checks do more than confirm measurements. A careful supplier inspects burrs, flatness, hole alignment, and packaging so the parts arrive ready to install, not just technically within print. Those combined habits—practical tolerances, clear material history, stable finishes, early feedback, real capacity, and meaningful inspection—are what make a bracket supplier dependable over time.
Contact Us
Contact Person: Kristy Wu
Email: [email protected]
Tel/WhatsApp: 8613826954049
Website: https://www.dgbosi.com/