Motorcycle Parts Vertical Lift Plating Equipment: Finding a Reliable Exporter
2026-09-15
Most plating lines for motorcycle parts still rely on outdated barrel systems that leave coverage gaps on complex surfaces. Vertical lift plating equipment solves this, but only if the exporter knows how to engineer it for real production demands. That’s where Junda stands out—not with marketing claims, but with a track record you can verify.
What Motorcycle Parts Actually Need Vertical Lift Plating?
Vertical lift plating isn't a one-size-fits-all upgrade. The parts that benefit most are those subjected to repeated clamping forces or exposed to harsh environmental stress where stock surfaces degrade quickly. Fork tubes are the prime candidate: the lower stanchions see constant sliding friction and stone impacts, so a vertical lift plate adds a hard, low-friction layer that resists pitting and keeps seals tight. Likewise, brake caliper pistons and master cylinder bores gain from the same treatment, as the plated surface reduces micro-corrosion that can cause sticky lever feel or uneven pad wear.
Beyond suspension and hydraulics, engine internals like shift forks and selector drums often need vertical lift plating after machining. These components endure intermittent high-load contact, and a thin, uniform deposit restores dimensional accuracy while preventing galling. Swingarm pivot bolts and linkage pins are also underappreciated candidates: they rotate through small arcs under heavy load, so plating helps maintain a smooth bearing surface longer than bare steel or even anodized aluminum.
Finally, consider fasteners and small bracketry in high-vibration zones. Items like exhaust flange studs, subframe mounting bolts, and footpeg pivot pins can work loose or seize due to thread fretting. A vertical lift plate here adds a sacrificial, corrosion-resistant layer that reduces friction during assembly and disassembly, making routine maintenance less of a headache. In short, any part where surface integrity directly affects safety, feel, or service life is a solid candidate for this specialized finish.
The Hidden Costs of Choosing the Wrong Plating Line Supplier
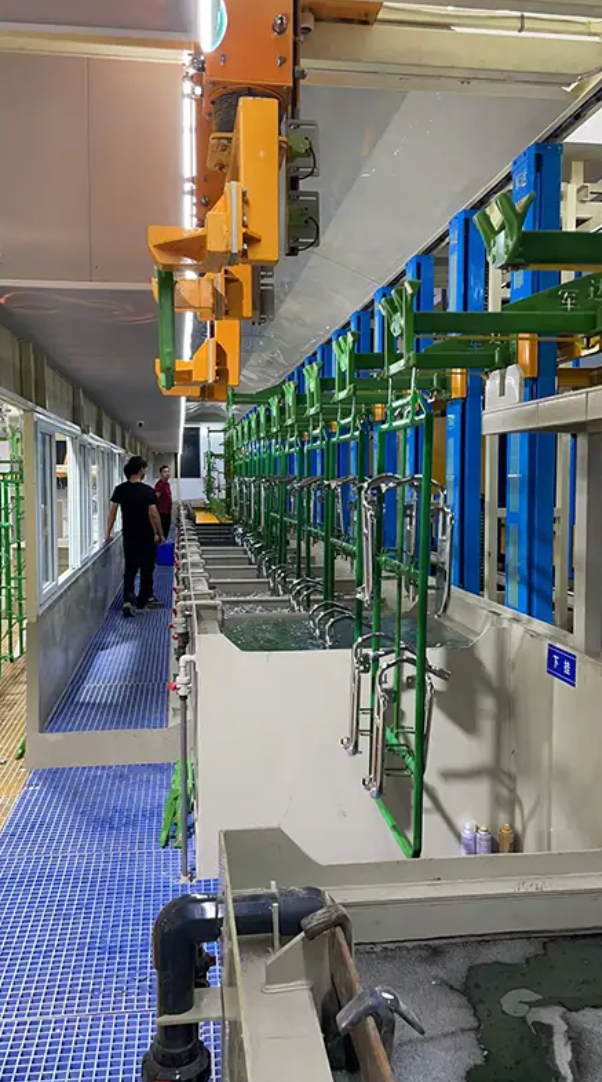
A plating line that arrives cheap rarely stays cheap. The first invoice might look attractive, but the real price shows up months later in ways that never made it into the quote. Thin tank walls bow under heat cycling, bus bars sized for someone else's amperage run hot, and rectifier cooling loops clog because the water quality at your site was never part of the conversation. Each fix feels small—a new gasket here, a reinforced brace there—until the maintenance log reads like a second mortgage.
Then there's the downtime you don't plan for. A line built without realistic time-motion studies leaves operators waiting on hoists that can't keep pace with the bottleneck station. Racks get redesigned on the fly, bath chemistry drifts because the filtration circuit was undersized, and the reject rate climbs quietly. Scrap and rework are not line items on the supplier's proposal, but they become the dominant operating cost within the first year, often dwarfing the initial savings.
Compliance and documentation are the quiet killers. A supplier unfamiliar with your region's wastewater discharge limits will happily sell you a line that dumps more chelates than your treatment system can handle. Retrofit costs for additional rinse stages, larger evaporators, or segregated waste streams land on your desk without warning. And when the audit comes, missing weld maps, material certifications, and coating thickness records turn a routine inspection into a stop-work order. The wrong supplier doesn't just deliver a line—they deliver a stream of unplanned capital requests.
Reading Between the Lines of Exporter Claims
When an exporter boasts about "premium quality" or "unmatched reliability," the real story often hides in the details they omit. Terms like "export-grade" or "internationally certified" can mean wildly different things depending on the market, and without digging into actual specifications or third-party test reports, buyers are left to trust a sales pitch rather than verifiable facts. A claim of "100% satisfaction guaranteed" is meaningless if the warranty fine print excludes almost every likely failure mode. Savvy importers learn to treat every superlative as an invitation to ask: compared to what, measured by whom, and documented where?
Another layer of obfuscation comes from vague references to "world-class standards" or "used by leading brands." These phrases imply endorsement without naming any actual standard body or brand partner, because doing so would expose the lack of formal certification or contractual relationship. An exporter might claim their factory "follows ISO 9001 principles" while never having passed an external audit — the phrase is technically true in spirit but legally hollow. Reading between the lines means converting such fuzzy language into a checklist of hard requirements: request the audit report, ask for a sample batch with traceable lot numbers, and verify the factory's export history through customs data rather than marketing brochures.
The most dangerous gaps often appear around what is not said at all. If an exporter lists only positive attributes and avoids mentioning rejection rates, lead time variance, or after-sales support capacity, those omitted areas deserve the most scrutiny. A claim like "fast delivery" without specifying the actual port-to-port time, whether it applies to full containers only, or what penalties apply for late shipment is essentially noise. Experienced buyers read exporter claims as a map of blind spots: each confident statement marks a territory worth a site visit, a reference check, or a trial order with carefully defined acceptance criteria.
A Practical Checklist for Evaluating Vertical Lift Equipment Build Quality
Start by looking at how the main frame is put together. Run your hand along the welds where the mast sections join the base and carriage—they should be consistent, without undercut, porosity, or random tack welds hiding misalignment. Check if reinforcing gussets are used at high-stress corners, or if the manufacturer just relied on a single fillet weld. Bring a straightedge and feeler gauge to check for gaps between bolted flanges; more than a millimeter or two often means poor jig alignment during fabrication. Also ask for the actual steel grade and plate thickness on the columns and fork carriage. A lift rated for 2,000 kg should not use the same thin-wall tubing as a 500 kg unit, even if the powder coat makes both look the same.
Next, spend time on the safety hardware and controls. Cycle each limit switch by hand and watch the response—does the carriage stop smoothly, or does it slam into the stops before the switch trips? Test the emergency stop and the manual lowering valve under partial load, not just empty. Hydraulic lifts should have a velocity fuse or hose burst valve directly on the cylinder, not just a check valve at the pump. Open the electrical panel and look for wire routing: zip-tied bundles with labeled terminals and proper strain relief are a good sign. Loose spade connectors, undersized fuses, or a nest of unlabeled control wires suggest the builder cut corners where few people look. If the unit has a folding guard or interlocked gate, make sure the interlock actually breaks the motion circuit instead of just sounding a buzzer.
Finally, judge how the equipment will age after a few years of daily use. Inspect the surface finish on hidden areas like the underside of the platform and inside the mast channels—if there is no primer under the paint, rust will start there first. Grease fittings should be accessible without removing panels, and wear pads should be replaceable with standard tools. Ask for a spare parts list with actual part numbers, not just a generic manual. During a demo, load the lift to its rated capacity and run it through five or six full cycles. Listen for changes in pump pitch, watch for hydraulic weep at fittings, and check if the mast deflects more than a few millimeters side-to-side. Those details tell you more about build quality than any glossy brochure.
When Lead Times Go Wrong: Protecting Your Production Schedule
A delayed shipment of raw materials doesn't just shift one order—it quietly eats into the buffer you've built for every job downstream. Once lead times stretch, the usual fixes like expediting freight or squeezing suppliers start to fail because the problem is no longer a single late delivery. It's a slow erosion of the schedule you rely on daily.
Instead of reacting to each missed date, look at where your schedule is most exposed. Often the highest risk sits in components with few alternative sources or in processes that can't be shortened without sacrificing quality. By mapping those fragile points before a crisis hits, you can pre-approve secondary vendors, hold a small safety stock of long-lead items, or shift production sequencing to keep critical work moving while you wait.
The real protection comes from treating lead time as a range, not a promise. When a supplier says three weeks, plan for five—and communicate that internally so sales doesn't overpromise. Build recovery time into every milestone, and review the schedule weekly with the team that actually touches the floor. That way, when a lead time goes wrong, you aren't rewriting the whole plan—you're just activating the backup you already built.
Negotiating with Exporters Without Sacrificing After-Sales Support
When you sit down with an exporter, the instinct is to drive the unit price as low as possible. But if that pressure forces them to cut corners on after-sales support, you'll pay for it later in downtime and repair bills. Instead, treat warranty terms, spare parts availability, and response times as negotiable items with real monetary value—just like the product itself.
One practical approach is to put a number on the support you expect. Ask the exporter to commit to a maximum response window for technical queries, a guaranteed stock of critical spare parts in your region, and remote diagnostics before dispatching a technician. Then tie a portion of the final payment or a service retainer to meeting those benchmarks. If they refuse to write specifics into the contract, that's a red flag about their actual after-sales capacity.
You can also shift some risk back to the exporter without being confrontational. Propose a pilot period where after-sales performance is measured against agreed KPIs, and use that data to renegotiate extended warranty or service-level upgrades. Many exporters will accept this if they genuinely believe in their support network—and the ones who won't are usually the ones you'd regret signing with.
FAQ
Check their track record with similar machinery, ask for client references in the motorcycle industry, and confirm they provide clear documentation on build materials, electrical systems, and safety features. A dependable exporter will also walk you through their quality checks before shipment.
Vertical lift keeps parts suspended and moving through baths in a controlled sequence, which reduces the risk of trapped air bubbles and uneven coating. For small, oddly shaped items like brackets or foot pegs, this setup gives more consistent coverage than barrel plating.
Most vertical lift lines are built for zinc, nickel, chrome, or copper plating, and some can be configured for multi-layer finishing. The exact capability depends on tank layout, rectifiers, and the chemical resistance of the lifting frame, so you should match the line to your target finish.
Ask about the lifting capacity per flight bar, tank dimensions, rectifier output, cycle time, and the programmable logic controller brand. Also verify the frame material—stainless steel or coated steel—and whether the exporter includes fume extraction and heating options.
Request a live video walkthrough of the production floor, ask for recent inspection reports, and have them run a short plating test on sample motorcycle parts you send. A serious exporter will agree to a third-party pre-shipment inspection without hesitation.
Look for remote commissioning guidance, clear wiring and installation drawings, and a responsive technical contact for troubleshooting. Some exporters also offer on-site training or can recommend local service partners, which matters when the equipment is crossing borders.
Yes, many exporters will adjust the number of stations, tank size, or automation level to fit your floor space and daily output. Be prepared to share part drawings, expected thickness, and production volume so the line is sized correctly from the start.
Underestimating installation requirements, not confirming voltage and frequency compatibility, and skipping a clear packing list can all cause delays. Also agree on incoterms and who handles customs clearance, because a low quote means little if the equipment arrives damaged or without essential parts.
Conclusion
Sourcing vertical lift plating equipment for motorcycle parts means recognizing that not every component tolerates conventional barrel or rack lines. Long, heavy or geometrically awkward pieces—fork tubes, swingarms, exhaust headers, shock bodies and cast engine covers—demand a vertical lift system where carriers rise and fall through staged tanks without excessive sway or contact damage. A capable exporter should understand how these parts hang, what current densities their surface areas require, and how plating thickness distribution changes across a vertical stroke. Press them for concrete examples of lines they have shipped for two-wheeler manufacturers, not generic industrial installations. Ask how they handle tank rigidity, bus bar sizing, and hoist synchronization; if they cannot answer in detail, walk away.
The real cost of a weak supplier rarely shows up at the quote stage. It appears later as uneven chrome on a fork stanchion, burned deposits on caliper brackets, or a rectifier that drifts under load. Dig into exporter claims: request photos of operating lines, PLC brand and spare-part lead times, and names of clients who run similar part geometries. Build quality starts with steel thickness, polypropylene welding, and ventilation that actually captures mist, but after-sales support is where long-term value lives. Negotiate warranty periods, remote troubleshooting, and a guaranteed local service partner before you sign. If lead times stretch, ask for milestone inspections and hold back final payment until the line plates your own sample parts acceptably. Protect both schedule and support, because the cheapest exporter often becomes the most expensive when production stops.
Contact Us
Contact Person: hayyr
Email: [email protected]
Tel/WhatsApp: 8613082110525
Website: https://www.jundaelectroplating.com