China Iron Casting: Excellence in Modern Manufacturing
2026-09-21
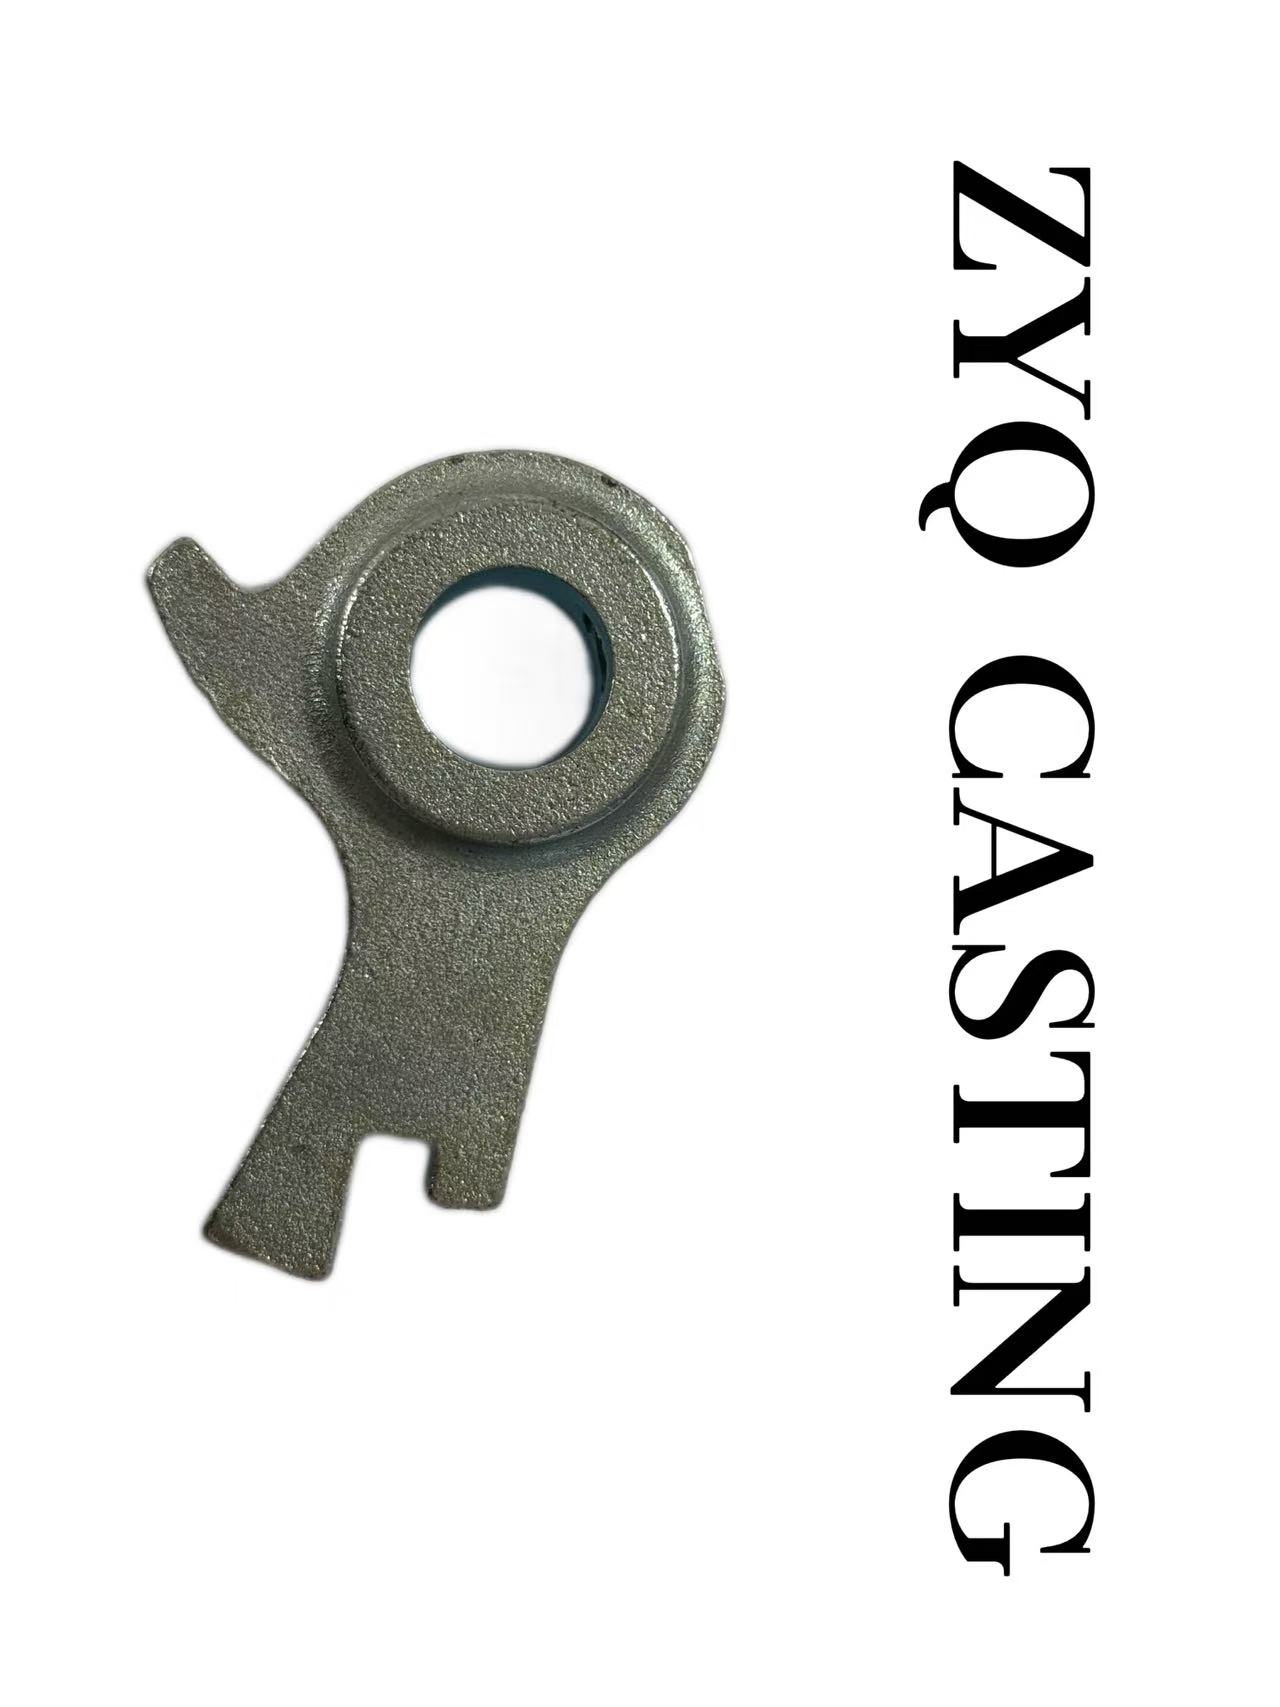
China’s iron casting industry has quietly transformed into a global powerhouse for precision components. But with thousands of foundries out there, how do you separate genuine excellence from empty promises? If you’ve ever wrestled with inconsistent porosity, late shipments, or vague material certifications, you know the pain. That’s why we’re turning the spotlight on Zhaoyuqi — a foundry that’s been methodically rethinking what modern ductile iron manufacturing should look like. From automated molding lines to rigorous in-house metallurgical testing, their approach hints at a bigger story about China’s manufacturing evolution. Let’s dig in.
Molten Metal, Measured in Microns
When a crucible tilts and a ribbon of liquid alloy spills onto a chilled wheel, the gap between the nozzle and the rotating surface often sits below a hundred microns. That distance is not a rough setting; it is the difference between a uniform amorphous foil and a splatter of wasted metal. Operators adjust the slit with feeler gauges and laser micrometers, because at pouring temperatures above a thousand degrees, thermal expansion of the frame can swallow a ten-micron tolerance before the first ingot has fully melted.
In thin-strip casting and precision coating, the molten metal is not simply poured; it is squeezed through a ceramic slot, dragged across a cooled substrate, or atomized through a nozzle whose bore diameter might be no wider than a few human hairs. Measuring the resulting film while it is still glowing requires non-contact sensors that ignore the heat shimmer. Eddy-current probes and confocal displacement meters track thickness in real time, feeding corrections back to the actuator that nudges the lip gap by a fraction of a turn.
Even in heavier foundry work, the same micron-level thinking shows up in mold alignment, core registration, and the final machining allowance left on a casting. A shift of twenty microns in a cope-and-drag setup can mean the difference between a part that cleans up with a light pass and one that gets scrapped for lack of stock. The paradox is familiar on the shop floor: you handle thousands of kilos of liquid metal, yet the quality decision is often made at a scale smaller than the grain of the alloy itself.
The Unseen Discipline Behind China's Cast Iron
In the foundries that still produce China’s most durable cast iron, the first discipline is silence. Raw pig iron and scrap are laid out on concrete floors and inspected piece by piece before dawn, when the low light makes impurities easier to spot. The molding sand is then packed by hand—not in haste, but in rhythmic layers, each one pressed until it resists with the same give as a ripe pear. Nothing about this stage is photographed or advertised; it is simply repeated until the hands know what the eyes cannot check.
The pour itself demands a focus that borders on ritual. Workers judge the molten iron by its color and flow, not by furnace readouts. A bright, almost white stream means the carbon is right; a sluggish orange means the pour will fail before the mold is full. In older workshops, the only sounds are the deep huff of the cupola and the crack of steam as hot metal meets damp sand. No one interrupts, because the window between too hot and too cold lasts less than a minute.
What makes the discipline truly invisible is the waiting. After casting, the iron is buried in ash or left in cooling sand for a full day—sometimes longer—while the crystal structure settles. Rushing this step would save hours and change nothing visible on the surface. But it is exactly this refusal to cut corners that gives the iron its even heat and resistance to cracking. The final piece carries no mark of that patience, yet it is the reason the pan or pot can outlive its owner.
Where Foundry Craft Meets Data-Driven Control
The heat in a foundry doesn’t care about dashboards. Neither does the pour, the cooling curve, or the subtle shift in sand moisture that turns a good casting into scrap. What we build here sits between that stubborn physical reality and the numbers that describe it. Sensors pick up what experienced hands already sense — a temperature drift, a change in melt viscosity, a slight delay in the knock-out cycle. The difference is that the data doesn’t stop at observation. It loops back into the process, adjusting variables before a defect ever takes shape.
That’s the quiet shift happening on the floor. It’s not about replacing the people who read a furnace by its sound or a mold by its color. It’s about giving them a second set of eyes that never blinks. The control layer we use doesn’t force a one-size-fits-all recipe onto every line. It learns the rhythm of a specific foundry — the quirks of its alloys, the lag in its cooling beds, the way a particular pattern behaves on a humid Tuesday. Then it starts making small, precise calls that keep that rhythm from breaking.
The result feels less like automation and more like intuition, sharpened. A foundry that runs this way still depends on craft. It just no longer has to choose between that craft and the kind of consistency that turns buyers into long-term partners. The melt stays within range, the pour stays calm, and the data doesn’t just tell you what happened. It helps you shape what happens next.
From Blast Furnace to Final Tolerance
The journey begins in the blast furnace, where iron ore, coke, and limestone descend into an inferno that strips away impurities and yields a molten river of raw steel. It is a violent, almost primordial process — yet within hours, that same seething metal is tapped, desulfurized, and alloyed with precision, carefully tuned to the carbon and manganese levels that will later define its strength and machinability.
From there, continuous casting shapes the steel into billets or slabs, and the rough edges of the foundry give way to controlled rolling and cooling. Each pass through the mill reduces thickness while refining grain structure, building a material that can withstand the stresses of reshaping. But true consistency only emerges when machining takes over: turning, milling, grinding — each cut brings the component closer to a dimensional blueprint measured in microns.
Finally, the part meets the metrology lab, where coordinate measuring machines and surface profilometers map every critical feature against design intent. The tolerance band is no longer an abstract limit but a physical boundary proven by data. What started as a furnace's violent chemistry now rests on an engineer's desk with a clean inspection report, ready for assembly — a quiet testimony to the discipline that lies between molten chaos and final precision.
Why Cast Iron Innovation Is Quietly Accelerating
Most people still picture cast iron as a brittle skillet or a rusty pipe, but inside foundries the material is being reworked at the microstructure level. Adjusting cooling rates, adding trace amounts of boron or niobium, and experimenting with compacted graphite morphologies has produced castings that are noticeably lighter and less crack-prone than the grade books from ten years ago suggest.
The push isn't coming from a single industry. Electric motor housings need better thermal conductivity and vibration damping without the weight penalty. Kitchenware brands want thinner walls that still hold heat evenly. Restoration architects keep demanding replacement parts that match century-old profiles but meet modern load codes. Each demand quietly feeds back into alloy recipes and sand-mold coatings, often without any public announcement.
What makes this acceleration easy to miss is that it rarely shows up as a breakthrough. It appears as revised material datasheets, tighter nodularity ratings, fewer porosity rejects, and machine shops noticing that a casting now drills cleanly instead of chipping. That iterative, unglamorous work is exactly how a supposedly mature material keeps finding new headroom.
Sourcing Logic: Beyond the Price Per Kilogram
When procurement teams fixate on the per-kilogram cost of raw materials, they often miss the hidden economics that shape long-term value. A lower upfront price can conceal higher scrap rates, inconsistent batch quality, or delivery delays that ripple through production schedules. Instead of treating sourcing as a simple transaction, experienced buyers evaluate suppliers on total cost of ownership: how well the material performs in a specific process, how predictable the supply chain remains under stress, and whether technical support arrives before a problem escalates.
This broader logic also weighs the stability of specifications rather than averages. Two suppliers may quote identical prices per kilogram, yet one delivers material with tighter tolerance ranges and fewer outliers. Tighter consistency means less adjustment on the line, fewer rejected lots, and more reliable output. Over a quarter, those differences dwarf a marginal price gap. Smart sourcing starts with a clear definition of what actually drives cost inside the plant, not just what appears on the invoice.
Finally, the relationship behind the quote carries value that no spreadsheet captures. A supplier willing to hold safety stock, share demand forecasts, or adjust formulations for a new product line reduces downstream risk. Price per kilogram remains an important signal, but it becomes meaningful only when placed beside quality history, lead-time reliability, and the supplier’s capacity to solve problems collaboratively. In that sense, sourcing logic is less about finding the cheapest kilogram and more about engineering the most dependable flow of material.
FAQ
A deep supplier network, skilled workforce, and steady investment in foundry automation allow Chinese manufacturers to handle both high-volume runs and intricate custom parts with dependable consistency.
Many foundries now use digital simulation, automated molding lines, and real-time temperature monitoring. This reduces defects and shortens lead times, especially for complex geometries that used to require multiple trials.
Automotive, agricultural machinery, pumps and valves, railway components, and construction equipment are among the biggest buyers. Their demand for durable, cost-effective parts keeps the sector tightly integrated with global supply chains.
Spectrometer analysis of molten metal, X-ray or ultrasonic inspection for internal flaws, and dimensional checks with coordinate measuring machines are typical. Many factories also document every batch for traceability.
Modern plants use dust collection systems, sand reclamation, and waste heat recovery. Older facilities have been pushed to upgrade or close, so the remaining capacity is generally cleaner and more efficient than a decade ago.
Yes. While China is known for mass production, a growing number of foundries specialize in short runs, rapid prototyping, and tooling adjustments. This flexibility suits equipment manufacturers needing replacements or small-batch components.
Gray iron and ductile iron dominate, with compacted graphite iron gaining ground for high-strength engine and brake parts. Each type offers a different balance of machinability, vibration damping, and tensile strength.
The combination of competitive pricing, mature logistics networks, and the ability to consolidate multiple parts in one shipment often offsets lead time concerns. Strong communication platforms also make remote project management easier than many expect.
Conclusion
China's iron casting sector has moved far beyond brute force. In modern foundries, molten iron is poured and then controlled to tolerances measured in microns—an exactness that redefines what this ancient material can do. The real story isn't just heavy machinery; it's the quiet discipline behind each pour. Foundry craft passed down through generations now meets data-driven process control: thermal sensors, spectrometers, and real-time dashboards track chemistry and cooling curves. From blast furnace to final machined surface, every variable is logged and adjusted, shrinking variation that used to be accepted as inevitable. This fusion of tactile skill and digital oversight is why cast iron parts from China increasingly match or exceed expectations in automotive, hydraulic, and industrial equipment markets.
Innovation is accelerating quietly, not through loud announcements but through iterative gains in metallurgy, mold design, and energy efficiency. Sourcing logic has matured beyond price per kilogram. Buyers now weigh dimensional stability, machinability, microstructure consistency, and a supplier's ability to document process capability. A foundry that can show Cp and Cpk values, melt traceability, and non-destructive testing records offers a different kind of value—one that avoids downstream failures and rework. China's iron casting excellence, then, is less about being the cheapest and more about being predictably good: repeatable pours, tighter tolerances, and a manufacturing culture that treats a two-thousand-year-old material with laboratory-grade seriousness.
Contact Us
Contact Person: Nico Yin
Email: [email protected]
Tel/WhatsApp: 8618561567088
Website: https://www.ductileironparts.com/