China Industrial Vibration Motor Selection Guide for Optimal Performance
2026-10-28
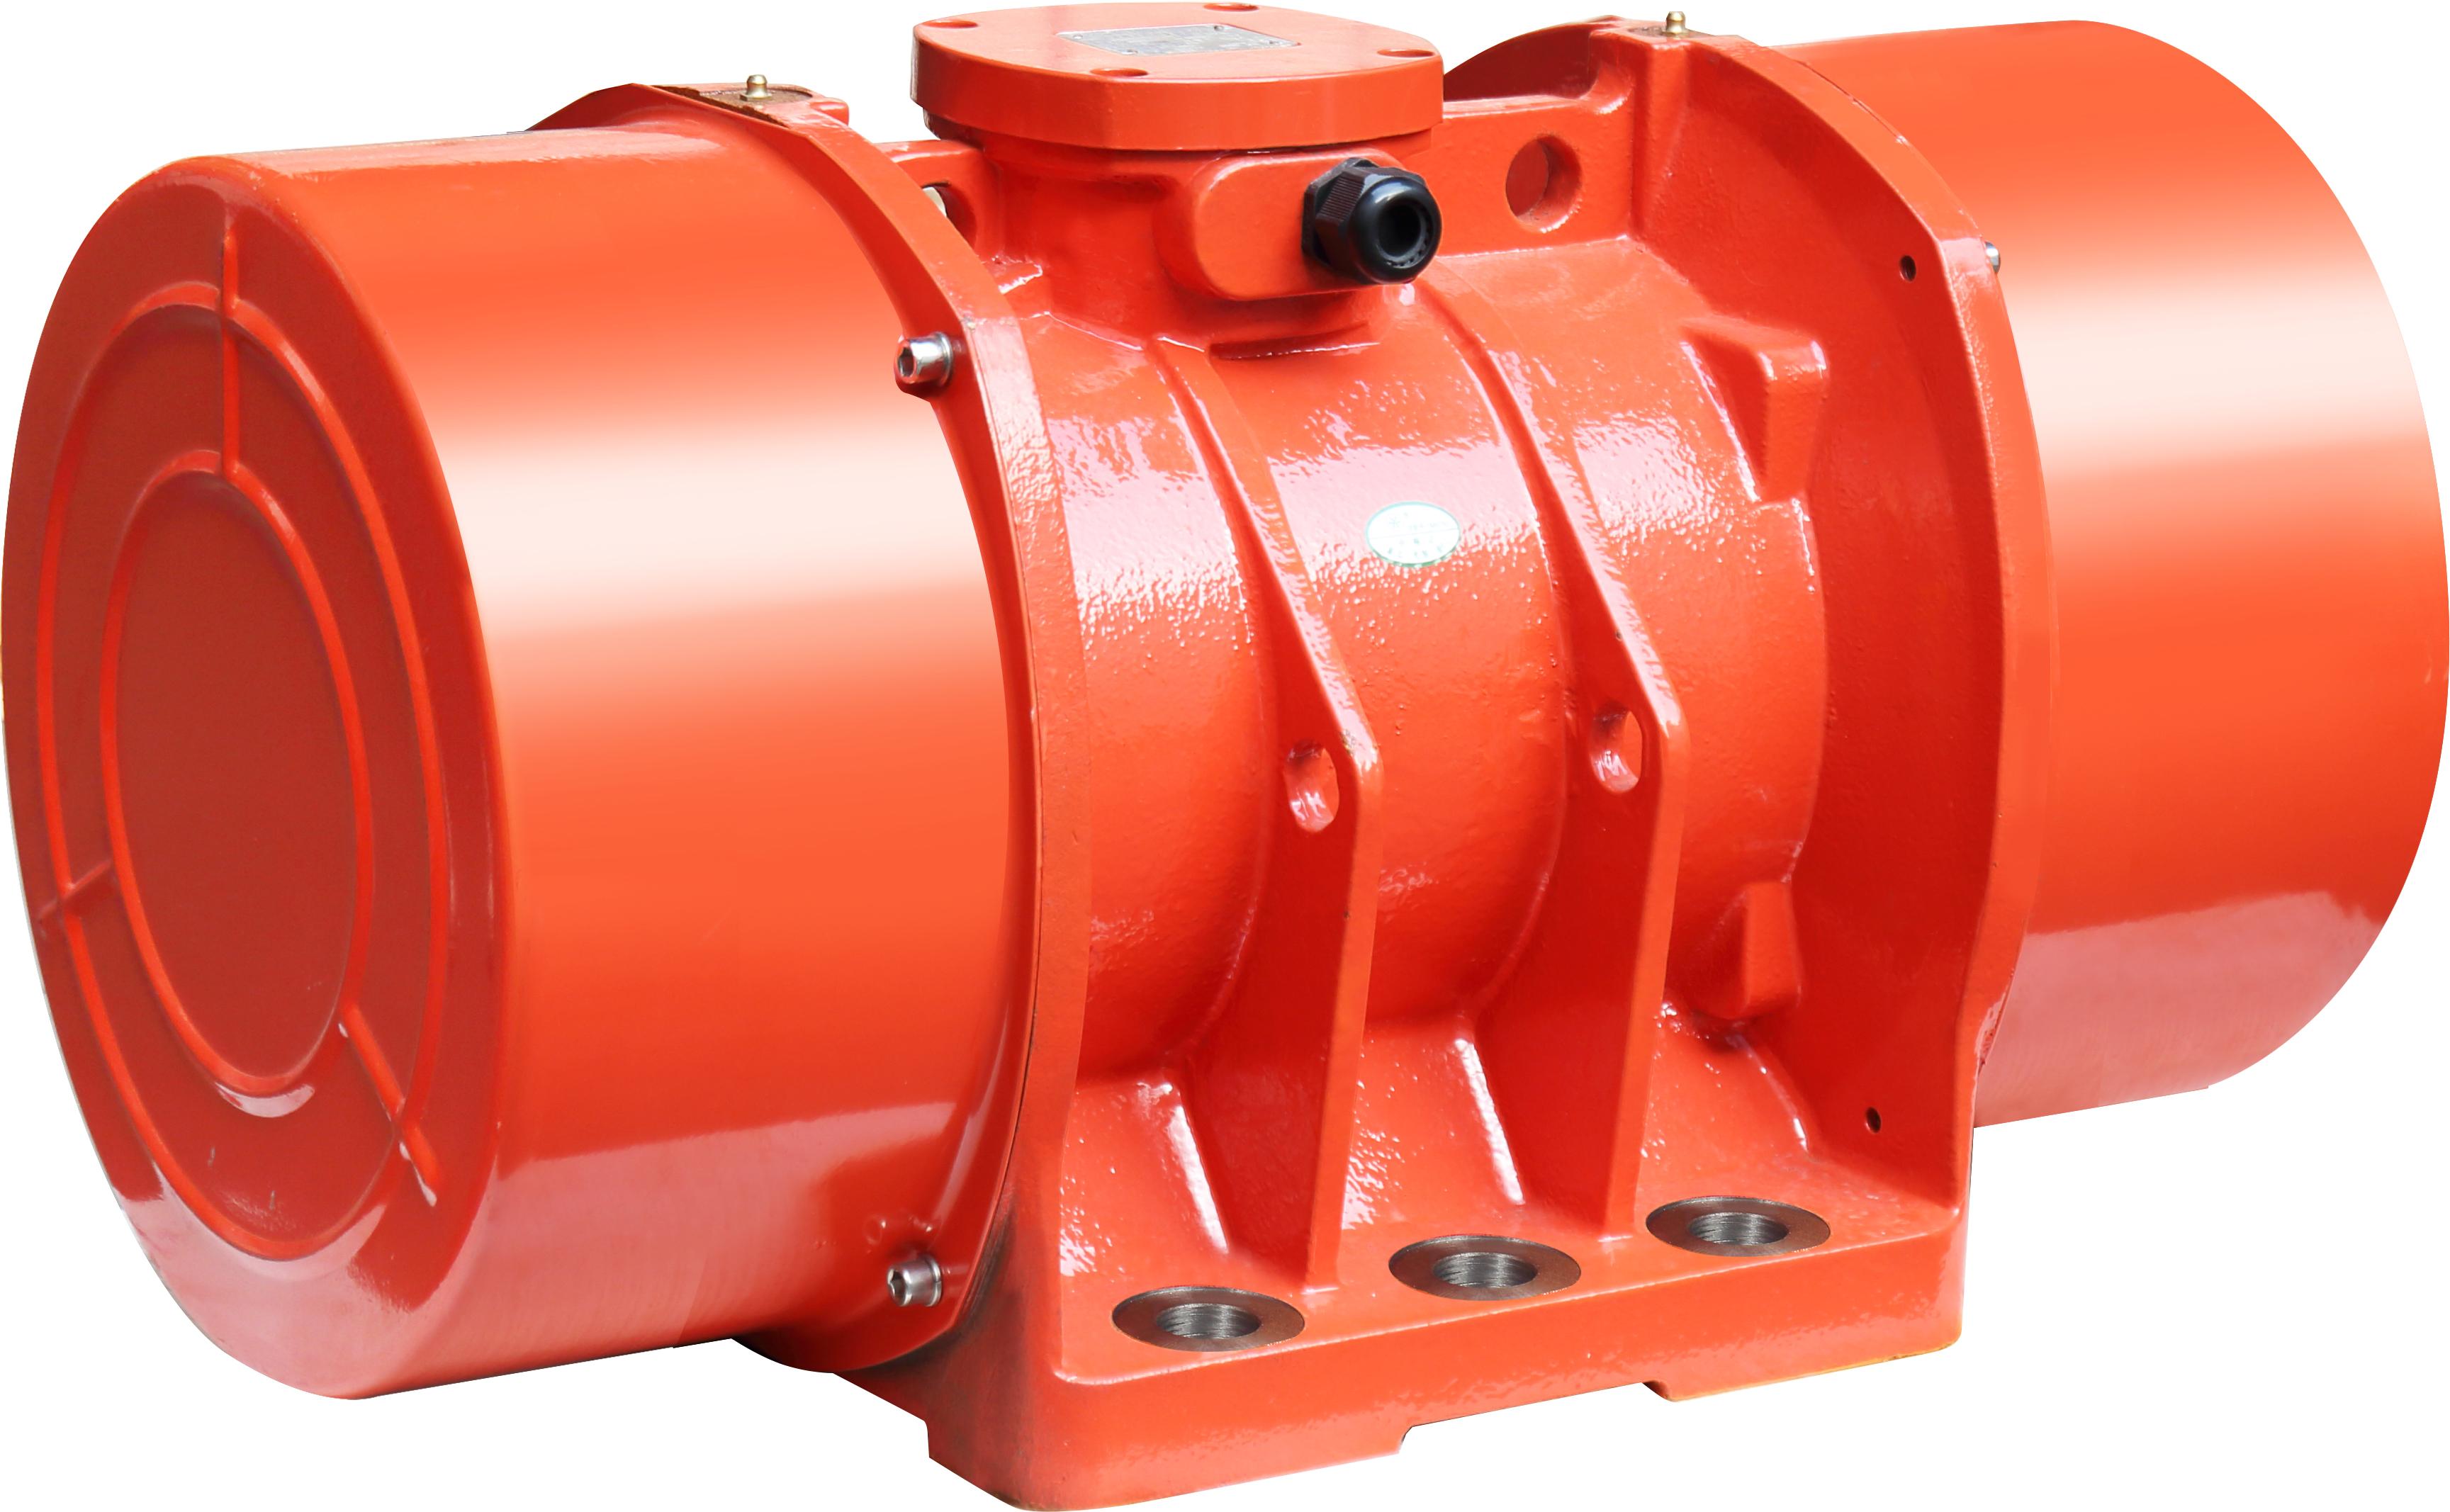
Selecting the right industrial vibration motor is rarely a one-size-fits-all decision. With countless specifications around force, frequency, and mounting, even seasoned engineers can overlook the subtle factors that quietly erode performance. This guide cuts through the noise, focusing on what actually matters for your application. As a trusted name in the field, Guangling has seen too many projects stall from avoidable mismatches—so let’s make sure yours isn’t one of them.
Pin Down How Your Bulk Material Actually Moves
Bulk solids rarely behave the way a datasheet suggests. A quick angle-of-repose test might tell you something, but it won't reveal how the material slumps, segregates, or sticks once it's in a hopper with a running feeder. You need to watch it move under conditions close to your actual process—same moisture, same particle size distribution, same consolidation pressure.
Run small-scale shear tests and bin discharge trials instead of relying on generic flow classifications. Pay attention to transition zones: the moment flow switches from mass flow to funnel flow, or when a bridge forms and collapses. These are the details that determine whether your equipment will handle Monday morning startup with damp material or a fresh batch from a different supplier.
Track how the material reacts after sitting still. Time at rest can build strength in powders and wet granules, turning a free-flowing solid into a stubborn arch. If you measure flow properties after consolidation and after storage, you'll spot problems that a one-time flow test misses.
The Force and Frequency Balancing Act
Think of a shaft spinning up through its critical speed: the forcing frequency sweeps across the natural frequency, and for a moment the two are locked in a dangerous embrace. That crossing is the heart of the balancing act—not avoiding the intersection, but managing how long and how violently the system lingers there.
Stiffness and mass set the natural frequency, while operating speed sets the force frequency. Changing either side shifts the ratio. But the choice isn't free: adding stiffness often adds mass, and lightening a component can lower its fatigue life. The balancing act means accepting trade-offs rather than chasing a perfect number.
Damping plays a quieter role. It doesn't change the frequencies; it changes how sharply the system responds near resonance. A well-damped mount can buy enough margin to survive a rough startup or a load spike, but too much damping wastes energy and can overheat. The real art is recognizing that the balance point drifts with bearing wear, thermal expansion, and even foundation settling—so the act is never truly finished.
Verify Chinese Supplier Claims Without a Factory Visit
Confirming a supplier's claims from afar starts with requesting live video walkthroughs of their production floor, raw material storage, and quality control stations. Ask them to show specific machinery you expect for your product category, and have them pan to a current newspaper or handwritten date code to prove the footage is recent. Pay attention to inconsistent background details—like mismatched signage or equipment that shifts between calls—which often signal a trading company posing as a factory.
Next, cross-check their export history and certifications through independent databases rather than relying on scanned documents they provide. For ISO or BSCI certificates, go to the issuing body's official portal and search by the certificate number. Likewise, plug their business license number into China's National Enterprise Credit Information Publicity System to see registered scope, operating status, and any past penalties. A factory claiming ten years of experience but registered only two years ago should raise immediate red flags.
Finally, order a pre-production sample with customized, hard-to-fake features—such as a unique logo placement, a non-standard color blend, or a specific packaging barcode—and have it shipped directly to you or a third-party inspector. Combine this with a remote video inspection where an independent auditor uses your checklist to verify raw materials, work-in-progress, and finished goods before shipment. The key is layering multiple verification methods so no single claim goes unchecked.
IP Ratings Alone Won't Save You in Dusty, Wet Environments
A high IP rating looks impressive on a spec sheet, but it only tells part of the story. Those tests are conducted in controlled laboratory settings, using specific dust particle sizes, water spray angles, and durations. Real-world industrial environments throw in variables the lab can't replicate: fine conductive dust that settles into connectors, condensation caused by rapid temperature swings, and water mixed with oils or cleaning chemicals. That IP67 enclosure might survive a 30-minute dunk in clean tap water, yet fail within weeks when exposed to a constant mist of slightly acidic coolant.
What actually kills equipment in harsh settings is rarely a single dramatic splash. It's the slow accumulation of micro-particles working their way past worn seals, the capillary action drawing moisture along cable jackets, and the pressure differentials caused by heat cycling that suck humid air inside. Even a perfectly gasketed enclosure can develop leaks at the entry points for cables or connectors—points the IP test doesn't fully stress. Without adding positive pressure, desiccants, or conformal coating to the internal electronics, you're relying on a rating that assumes ideal gasket compression and zero material aging.
The smart approach treats the IP number as a baseline, not a guarantee. Inspect seals after every maintenance cycle, route cables with drip loops, and consider potting or nano-coating for boards that see condensation. In dusty or wet environments, success comes from design details that go beyond a splash test—things like angled connector faces, breather vents with hydrophobic membranes, and regular visual checks for seal compression set. Otherwise, you're one compromised O-ring away from a failure that no IP rating could have predicted.
Match Voltage, Phase, and Duty Cycle to Your Production Line
Line voltage that looks fine on paper often drops under load once the equipment starts cycling. Before you commit to a machine, measure the actual supply at the panel during peak production hours—not just at startup. A 208V nominal feed can sag below the equipment's tolerance when other stations pull current, and that gap shows up as inconsistent welds or premature contactor wear.
Phase balance matters just as much for three-phase units. If your facility shares a transformer with heavy motor loads, check the leg-to-leg voltages while those motors are running. An imbalance over 2–3% will force the control board to compensate or simply fault out. Duty cycle often gets overlooked until a shift runs long: a 50% rating at full output may be fine for prototype work but not for continuous indexing. Size the cooling and the electrical service around the worst hour you actually expect to run, not the average.
Why Cheap Bearings and Weak Mounts Sink Long-Term Reliability
It's easy to look at a spec sheet and think a budget bearing will hold up. But once it's pressed into a mount that flexes under load, the whole assembly starts eating itself. Cheap bearings often have inconsistent raceways and softer steel, so the first few hundred hours feel fine before micropitting shows up where you can't see it.
Weak mounts make this worse. If the housing twists or shifts, the bearing no longer sits square. That misalignment concentrates stress on the edges of the rollers or balls, accelerating wear and generating heat. Pretty soon the grease breaks down, clearance opens up, and vibration travels into the surrounding structure—turning a small cost saving into a recurring maintenance problem.
Long-term reliability isn't about surviving a test bench; it's about tolerating real-world misalignment, temperature swings, and shock loads without degrading. Skipping quality on bearings and mounts may not show up on day one, but it shows up in every unexpected shutdown, every replacement cycle, and every hour of lost production later on.
FAQ
Focus on the required centrifugal force and working moment, not just motor power. Confirm the screen's total vibrating weight, amplitude target, and operating speed, then match those to the motor's eccentric weight settings and RPM. Also verify the mounting foot dimensions and bolt hole spacing against your existing frame.
Use the formula F = m × e × ω², where m is the eccentric mass, e is the eccentricity, and ω is the angular velocity in radians per second. For hopper discharge, aim for a force roughly 2.5 to 3.5 times the weight of the material plus the hopper section being vibrated. Always add a 15-20% safety margin to account for material bridging.
Most Chinese manufacturers offer windings for 60 Hz, but you must specify it at order time. The motor's speed increases by 20% at 60 Hz compared to 50 Hz, which raises vibration force significantly. Request the force and current draw curves at both frequencies and ensure the bearings are rated for the higher RPM.
Four common options are foot-mounted, flange-mounted, vertical with a protective hood, and through-bolt mounting. Foot-mounted units work for retrofits, flange types reduce overall height, vertical mounts suit compact spaces, and through-bolt designs simplify attachment to chutes. Always confirm the mounting hole tolerance to prevent stress cracking.
Request a factory audit video, not just a brochure. Ask for material certificates for the rotor and stator laminations, bearing brand and grade, and a sample test report showing insulation resistance and vibration amplitude. A reliable supplier will also provide a thermal test at rated duty cycle and give a clear warranty covering bearing failure and winding burnout.
Most industrial vibration motors have adjustable eccentric weights at both ends. Repositioning the weights changes the overlap angle and therefore the amplitude and force. For directional vibration on feeders, set the two weights to the same angle; for circular motion, offset them. Always make the same adjustment on both ends and re-tighten the clamping bolts to the specified torque.
Specify at least IP65 with an F-class insulation system and a corrosion-resistant paint finish. Dust can block cooling fins and enter the terminal box, so ask for a sealed terminal box with a cable gland and an internal condensation drain plug. For outdoor use, add a rain canopy over the motor if it is mounted vertically.
Check the nameplate for S1 duty rating, which means continuous running at full load without derating. Many vibrator motors are S2 or S3 for intermittent use, and using them continuously will overheat the windings. Request a temperature rise test certificate at the motor's maximum force setting and compare the measured winding temperature to the insulation class limit.
Conclusion
Before you even look at a catalog, spend time watching how your bulk material actually moves. A fine powder that aerates will behave nothing like wet sand or lumpy aggregates, and that difference dictates whether you need a compact high-frequency drive or a slower, higher-amplitude unit. Once the material's behavior is clear, force and frequency become a balancing act. A motor that produces impressive centrifugal force on paper can shake a lightweight hopper to pieces without moving much product, while too little force leaves material sitting dead on the screen. The useful combination is one where the force holds up under your real operating RPM, not just the peak number printed on a label.
When dealing with Chinese suppliers, remote verification matters more than glossy datasheets. Ask for a video of the exact model running under load, or request a detailed test report with dated photos. If a factory won't provide that, the claimed specs aren't worth much. Ratings like IP65 also need closer scrutiny: a high number doesn't guarantee survival in dusty cement plants or daily washdowns if the shaft seal, cable gland, and coating are weak. Match the motor to your actual voltage, phase, and duty cycle, because a motor rated for intermittent use will overheat on a continuous production line. Bearings and mounting feet deserve just as much attention. Cheap bearings with the wrong grease and thin castings that crack after repeated starts are the hidden reasons many imported motors fail early, even when their headline numbers look fine.
Contact Us
Contact Person: ZHUO
Email: [email protected]
Tel/WhatsApp: 86-576-86320988
Website: https://www.cnguangling.com